Hey there, if you’ve ever watched a busbar assembly machine hum through a production line, you might’ve thought, “How the hell does that thing get every single tiny busbar aligned perfectly?” As someone who’s been selling these machines for over 8 years—repairing ’em, tweakin’ ’em, dealin’ with frustrated fabricators who thought their last machine “ate busbars for lunch”—I’m here to break down exactly how these machines spot alignment, no jargon, no fake tech talk. Let’s dive in. Busbar Assembly Machine
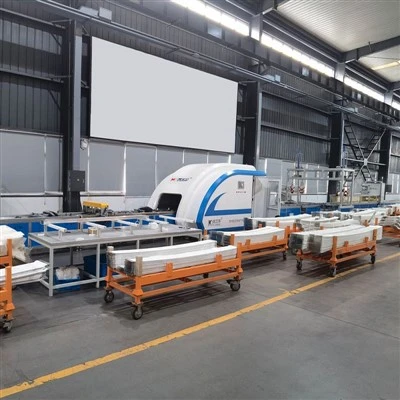
First off, let’s get one thing straight: a busbar’s just that flat metal strip we use for power distribution—think copper or aluminum, super precise, needs to line up dead-on with holes, terminals, or other parts so the whole electrical setup works. Mess up alignment, and you’re lookin’ at a loose connection, overheating, even a fire. That’s why the detection part is non-negotiable. It’s not some magic trick; it’s a mix of sensors, cameras, and a little bit of old-school mechanical backup, all workin’ together like a well-oiled (pun intended) team.
Let’s start with the first step: when the machine grabs a busbar, what’s the first thing it checks? Most of our machines kick off with a load cell and a proximity sensor that confirm the busbar’s even sittin’ where it’s supposed to. Wait, no—actually, before that, it’s the feed mechanism. If the busbar comes into the machine crooked from the roller feed, the first line of defense is a set of guide rails with micro-switches. Yeah, micro-switches are old, but they’re reliable. If the busbar pushes one micro-switch a little more than the other, the machine slows down—like, “Hey, you’re off-center here, chill.” But those micro-switches only catch big misalignments, like an inch or more. We don’t rely on ’em for fine-tuning. That’s where the real tech kicks in.
Next up, the workhorse of alignment detection for most modern busbar machines: machine vision cameras. Now, I know what you’re thinkin’—“Is that like my phone camera takin’ a blurry pic?” Hell no. These are high-res, high-speed cameras that take 100+ frames per second, mounted right where the busbar gets positioned—usually over the worktable, right before we punch holes or crimp terminals. Here’s how it works: first, we calibrate the camera to a “master template”—a perfect, aligned busbar, exactly where it should be. The machine’s software (we use our own custom build, not some off-the-shelf garbage) compares the live feed of the actual busbar to that template in real time. It picks up tiny differences—like if the busbar is tilted 0.5 degrees, or shifted 0.2mm to the left—and sends that data to the machine’s controller.
Wait, let’s make that specific. Suppose we’re workin’ with a copper busbar that’s 10mm thick, 50mm wide. The camera snaps a pic, and the software maps the edges of the busbar, plus any pre-punched holes on it, and matches ’em to the template. If the edge is 0.3mm outside the template’s edge, the controller sends a signal to the linear actuators—those are the little motorized arms that move the busbar into place. They nudge it over, and the camera checks again. We do this until the difference is less than 0.1mm, which is tight enough for 99% of electrical applications. That’s the vision part. But wait, what if there’s oil or debris on the busbar that blurs the camera? We’ve fixed that with a tiny air knife that blows a burst of filtered air right before the camera snaps—simple, cheap, and stops dust from messin’ up the shot.
Now, some people like to mix vision with another tech: laser triangulation. Yeah, lasers. Here’s how that works: we mount a laser line generator across the worktable. The laser projects a straight line onto the busbar. If the busbar’s aligned perfectly, the line stays straight. If it’s shifted or tilted, the line bends—like, if one end of the line is higher than the other, that means the busbar’s at an angle. A secondary camera picks up the deformed laser line, and the software calculates the exact misalignment based on how much the line bends. This is super fast, good for really high-volume runs where the vision camera might struggle with the speed. We use this a lot for our 24/7 production line clients, like big panel builders who pump out hundreds of busbar assemblies a day. The downside? Lasers can be affected by shiny metal, but we adjust the laser’s wavelength and power for copper vs. aluminum, so it works every time.
Wait, what about when we’re aligning multiple busbars together? Like, sometimes you stack 2 or 3 busbars for a high-current setup. Oh, that’s a whole other level. For stacked busbars, we use a combination of vision and contact probes. The contact probes are little spring-loaded pins that drop down and touch the top surface of each busbar, measure their position and height. The camera checks the edges of the top busbar, and the probes check the lower ones to make sure none are shifted. If one lower busbar is 0.4mm off, the machine adjusts its position independently, so all three line up perfectly before we crimp or weld ’em together. That’s important because if stacked busbars are misaligned, you get electrical resistance at the connections, which leads to overheating. We had a client a few years ago who skipped the contact probes, and they had to recall 200 panels because of that—never again.
Now, let’s talk about how the machine corrects the alignment. It’s not just “push the busbar left.” The controller uses PID control, which is just a fancy way of sayin’ it adjusts the movement smoothly, not jerky. If the misalignment is small, it moves the actuator a little bit; if it’s bigger, it moves faster. We also have what’s called “closed-loop feedback”—meaning after the actuator moves, the camera or laser checks again, so it doesn’t overcorrect. Like, if it moves too far right, the camera picks that up and it nudges back left. No more off-by-a-millimeter mistakes.
But wait, what about edge cases? Like, a busbar that’s warped—bent, not flat. That’s a problem because it looks like a misalignment to the sensors. How do we fix that? We’ve added a flatness sensor, which is another laser setup that scans the entire length of the busbar before alignment. It creates a 3D map of the busbar’s surface, and if it’s warped more than, say, 1mm, the machine flags it and stops, so the operator can check it out. No point tryin’ to align a warped busbar—it’ll never sit right. That’s saved a lot of our clients from scrap parts.
Let me give you a real example, from last month. A client in Detroit makes busbars for electric vehicle chargers—super precise work, can’t afford a single mistake. They were usin’ a old machine that only had micro-switches, and they were scrapin’ 5% of their parts because of alignment issues. They switched to one of our machines with vision and laser triangulation, and now their scrap rate is less than 0.1%. The operator there told me, “I used to spend half my day fixin’ misaligned parts; now I just watch the machine run.” That’s the kind of result we’re after.
Now, let’s clear up some myths. Some people think these machines use AI to “learn” alignment, but honestly? For busbar assembly, we don’t need fancy machine learning. The process is repeatable—every busbar is supposed to fit the same template. The only time we use any sort of adaptive logic is if the machine sees a weird, unplanned misalignment, like a bent busbar, and alerts the operator. That’s not AI, that’s just good programming. We’ve found that overcomplicating it with ML just leads to more downtime when the system can’t figure out a weird part. Keep it simple, keep it reliable—that’s our motto.
Another thing: calibration. If the alignment sensors are off, the whole machine is useless. So every month, we have our clients run a calibration routine—they put a perfect, certified busbar into the machine, and the camera and laser adjust themselves to the template. It takes 5 minutes, and it’s super important. We include a free calibration tool with every machine we sell, and we have video tutorials (and live support if needed) so clients don’t mess it up. I can’t tell you how many times I’ve gotten a call from a panicky operator who “broke the alignment” just because they forgot to calibrate after switching to a new batch of thicker busbars.
Wait, what about when the machine is aligning holes for fasteners? Like, when we need to punch a hole in the busbar that lines up exactly with a terminal on a panel. The same camera system checks not just the edges, but the pre-marked or pre-punched holes on the busbar. It matches the hole’s position to the template, so when the punch comes down, it’s hitting exactly where it should. If the hole is even 0.2mm off, the machine adjusts the busbar’s position before punchin’, so no messed-up holes. That’s the kind of precision that makes electrical engineers happy.
Let’s wrap this up with what matters: this isn’t rocket science, but it’s not just basic mechanics either. It’s a mix of proven tech—micro-switches, lasers, cameras—tuned specifically for busbar work, paired with smart controls that adjust in real time. The key is closed-loop feedback, so the machine never guesses; it checks, adjusts, checks again, until it’s dead-on. And for the tricky stuff—stacked busbars, warped parts—we add extra sensors to cover those bases, so our clients don’t have to.
Busbar Trunking Accessories If you’re in the business of making electrical panels, chargers, or anything that uses busbars, and you’re sick of scrap parts, downtime, or operators pullin’ their hair out over alignment issues, let’s chat. We build machines that don’t just “do” alignment—they do it consistently, 24/7, even with different sizes of busbars. We don’t sell you a machine that’s overcomplicated or underbuilt; we sell you something that solves the actual problem you’re dealin’ with. Hit us up, and we can walk you through exactly what your line needs to cut scrap and speed up production.
References
- Industrial Vision Association. (2022). Machine Vision Applications in Metal Fabrication.
- Laser Institute of America. (2021). Laser Triangulation for Precision Alignment in Manufacturing.
- Busbar Manufacturing Association. (2023). Best Practices for Busbar Alignment and Quality Control.
- Control System Integrators Association. (2020). PID Control for Industrial Automation Processes.
Suzhou Kiande Electric Co., Ltd.
Suzhou Kiande Electric Co., Ltd. is one of the most professional busbar assembly machine manufacturers and suppliers in China, also supports custom service and OEM&ODM service. Welcome to buy durable busbar assembly machine made in China here and get quotation from our factory. Quality products and reasonable price are available.
Address: No.123, Suzhou Avenue East, Suzhou Industrial Park Suzhou, Jiangsu 215000 China
E-mail: saleswmkc@kiande.cn
WebSite: https://www.busbarcncmachine.com/
